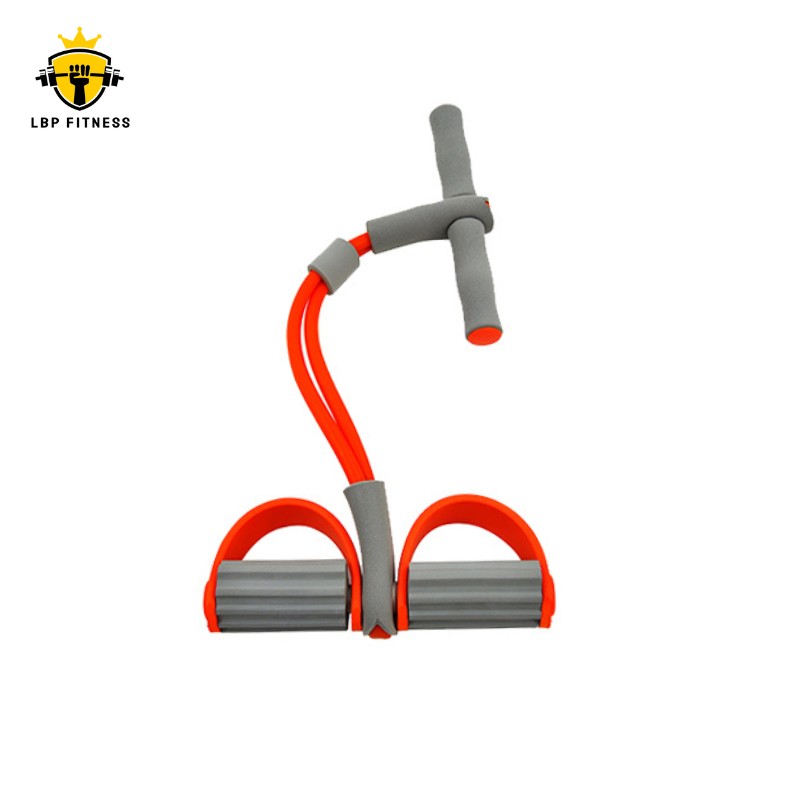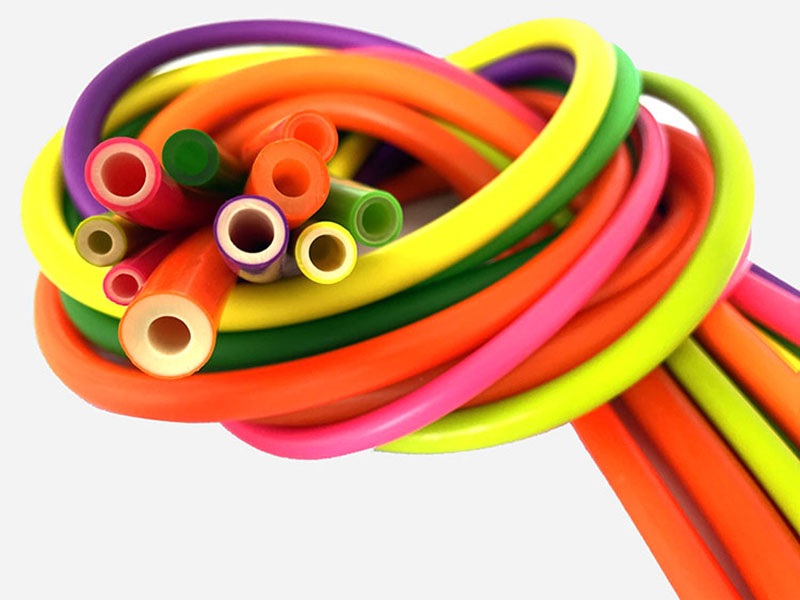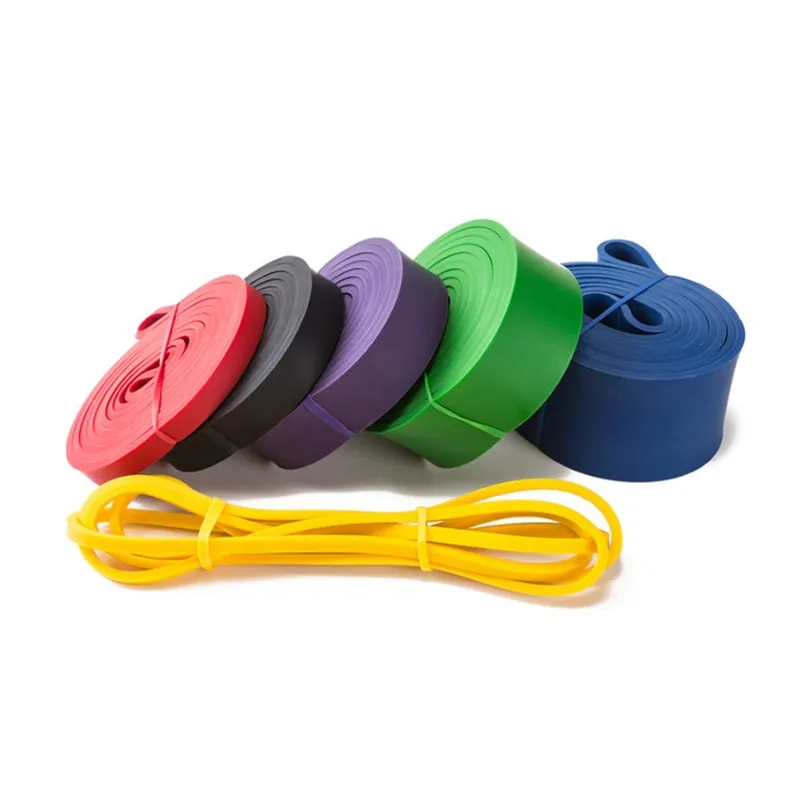
A resistance band can look correct and still be wrong for your market. The resistance may vary from the approved sample, a tube may pull out of its handle, a logo may transfer, or a barcode may be applied to the wrong strength level. For a private-label brand, those are not merely factory defects. They can become returns, poor reviews, rework, delayed inventory, or a safety incident carrying your name.
This is why quality control should begin before production, not at final inspection. A buyer and manufacturer need a measurable specification that defines how the product will be tested and what will be accepted.
The risk is real. In May 2026, the US Consumer Product Safety Commission announced a recall of HomeProGym resistance bands because the bands could forcefully separate from their handles. An earlier SPRI recall covered about 95,000 resistance bands and included reported injuries. These cases do not mean every band assembly is unsafe. They show why connection points, resistance levels, and fatigue requirements must be treated as engineering and procurement issues rather than marketing language.
Short answer
Before approving mass production, specify at least these items:
- product construction and material;
- resting dimensions and tolerances;
- target force at a defined extension;
- fatigue-test extension, cycle count, speed, and failure criteria;
- critical, major, and minor defects;
- logo, color, packaging, and barcode acceptance standards;
- sampling and lot-acceptance plan;
- records or photographs required before shipment.
A physical sample remains important, but it should support the written specification rather than replace it.
Why “heavy resistance” is not a specification
Band colors and labels such as light, medium, and heavy are convenient for users, but they are not universal engineering values. Two bands sold as “heavy” can produce different forces because of changes in material, width, thickness, loop length, construction, and extension.
The buyer should therefore define resistance as a force range at a stated extension. For example, the specification might require a band to produce an agreed force when stretched to 2x its resting length. The exact value should be based on the product design and target market rather than copied from another brand.
ASTM D412 is a useful reference for understanding tensile testing of vulcanized rubber and thermoplastic elastomers. It also provides an important warning: tensile results depend on factors such as extension rate, temperature, humidity, specimen geometry, and conditioning. Results should only be compared when the test conditions are equivalent.
The quality specification buyers should approve
The following table converts broad purchasing language into measurable requirements. It matters because each item needs both a target and a verification method; otherwise the buyer and factory may interpret the same approval differently.
| Quality item | What the buyer should define | How it can be verified | Risk if omitted |
|---|---|---|---|
| Material and construction | Natural latex, TPE, silicone, fabric blend, single layer, dipped, extruded, or assembled construction | Material record, approved sample, and supplier declaration | Different feel, elasticity, allergy positioning, or durability |
| Resting dimensions | Length/circumference, width, thickness, tube ID/OD | Caliper, thickness gauge, and length fixture | Incorrect fit and inconsistent resistance |
| Dimensional tolerance | LBP standard: width +/-5%; thickness +/-0.3 mm, unless an order specifies otherwise | Measurements across an agreed sample | Batch variation and resistance mismatch |
| Resistance | Force range at a stated extension, such as 1.5x, 2x, or another agreed point | Calibrated force gauge or tensile tester | Mislabelled levels and customer complaints |
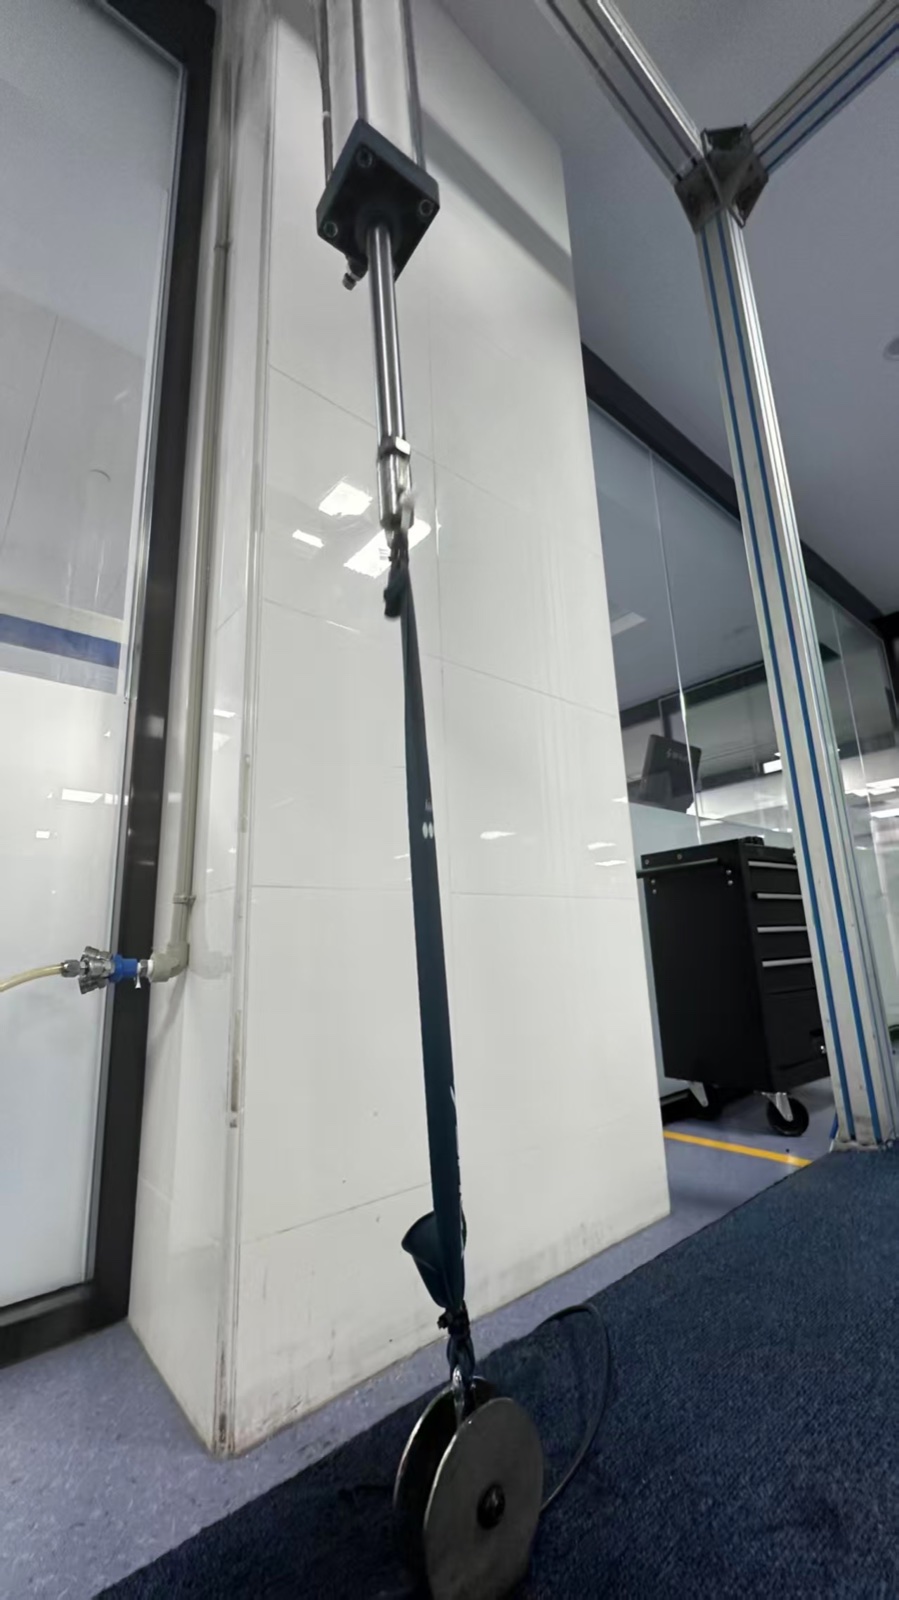
| Fatigue | Extension ratio, cycle count, rate, environment, and failure criteria | Cycle-test equipment and documented setup | Cycle numbers that cannot be compared |
| Assembly security | Pull-out or separation requirement for handles, D-rings, webbing, anchors, and clips | Static and/or cyclic assembly test | Recoil or impact hazard |
| Surface condition | Acceptable cosmetic characteristics and rejectable structural defects | Visual inspection under agreed conditions | Unnecessary rejection or unsafe acceptance |
| Printing | Artwork, location, color, adhesion, rub resistance, and transfer limits | Approved artwork, visual check, and rub/transfer test | Brand inconsistency and packaging contamination |
| Packaging | Fold, bag, insert, barcode, warning, SKU, carton, and quantity | Golden sample and packing audit | FBA, retail, or warehouse rework |
The buyer conclusion is simple: every important requirement should be expressed in a way that can be checked on the sample and again on the production lot.
How to write a meaningful fatigue-test requirement
A claim such as “tested for 20,000 cycles” is incomplete unless the test conditions are stated. Stretching to 1.5x resting length is not equivalent to stretching to 3x. Speed, temperature, specimen geometry, connection design, and the definition of failure also affect the result.
LBP’s current product-specific reference values include:
| Product | Approved fatigue statement | Important qualification |
|---|---|---|
| Power band loops | Minimum safety fatigue-test value: 20,000 cycles | Test extension is normally selected within 1.5x–3x resting length according to the specification |
| Resistance tubes | Tested up to 50,000 cycles | This is a maximum test result, not a universal warranty for every tube or assembly |
| Latex mini band loops | Tested to 70,000 cycles | The applicable extension, product dimensions, environment, and failure criteria must accompany the result |
These figures should not be used as interchangeable lifetime claims. A laboratory test helps compare products under controlled conditions; actual service life also depends on use intensity, overstretching, abrasion, storage, UV exposure, chemicals, attachments, and user inspection.
When requesting a fatigue test, define:
- the product and exact specimen dimensions;
- the resting gauge length;
- minimum and maximum extension;
- cycle rate;
- test temperature and conditioning;
- target number of cycles;
- failure criteria, such as rupture, permanent deformation, resistance loss, delamination, or connection separation;
- the record required, such as machine photographs and a result summary.
Cosmetic characteristics versus safety defects
Natural latex products can show minor color variation, surface texture, powder residue, tiny isolated bubbles, or superficial marks. Buyers need a defect reference that distinguishes these characteristics from cracks, dangerous thinning, delamination, contamination, or assembly failure.
The table below is not a substitute for the approved defect board, but it shows how the decision logic should work.
| Observation | Typical classification | Buyer action |
|---|---|---|
| Slight color variation that does not affect identification | Cosmetic/minor | Accept within the approved visual limit |
| Small isolated powder residue | Cosmetic/minor | Clean or accept if function and packaging are unaffected |
| Superficial mark that does not open during stretching | Cosmetic/minor | Compare with approved limit sample |
| Significant width or thickness outside tolerance | Major | Reject affected units or lot according to the inspection plan |
| Wrong resistance level, SKU, barcode, or artwork | Major; potentially critical to the order | Contain the lot and investigate traceability |
| Deep crack, tear, delamination, dangerous thinning, or foreign inclusion creating a stress point | Critical/safety-related | Do not release affected product |
| Tube, D-ring, handle, strap, anchor, or clip separation | Critical/safety-related | Stop release and perform root-cause and corrective-action review |
The buyer should conclude that “looks imperfect” and “unsafe” are not synonyms. A clear defect standard protects users while preventing subjective disputes over harmless characteristics.
What AQL does—and does not—mean
ISO 2859-1:2026 defines sampling schemes indexed by acceptance quality limit for lot-by-lot inspection. Instead of automatically inspecting every unit for every characteristic, an agreed plan determines how many units are sampled and the acceptance or rejection threshold.
LBP can publicly use the following defect-level references in an agreed inspection plan:
- critical defects: AQL 0.65;
- major defects: AQL 2.5;
- minor defects: AQL 4.0.
The exact sample size still depends on lot size, inspection level, sampling plan, and applicable switching rules. AQL does not mean that the stated percentage of defective products is deliberately shipped. It is a statistical lot-acceptance framework. Safety-critical controls may also require additional testing, process controls, or 100% checks depending on the product and contract.
When not to rely on a standard catalog specification
A catalog specification may be insufficient when:
- the band is part of a new training device;
- the product uses custom lengths, unusual wall thicknesses, or progressive resistance;
- a tube is assembled with handles, D-rings, anchors, or protective sleeves;
- the brand makes a precise resistance claim on its packaging;
- the product is intended for high-frequency commercial use;
- the buyer requires a new material, print system, or packaging configuration;
- regulatory, retailer, marketplace, or target-market requirements differ from the standard product.
In these situations, the buyer and manufacturer should create a project-specific specification and validation plan.
Common buying mistakes
- Approving only by appearance. A correct color and logo do not confirm resistance consistency, fatigue performance, or connection security.
- Comparing cycle counts without test conditions. A higher number can be less demanding if the extension ratio, speed, or failure criteria differ.
- Using color as the resistance specification. Colors are not universal and can lead to mislabelled sets, returns, or unsuitable training progression.
- Testing raw tubing but not the complete assembly. Handles, straps, D-rings, clips, and anchors can introduce failure points that a material-only test will not reveal.
- Leaving cosmetic limits undefined. This creates subjective disputes and can cause either unnecessary rejection or acceptance of a structural defect.
- Treating AQL as 100% inspection. Sampling inspection and unit-by-unit inspection are different controls and should be described accurately in the purchase agreement.
- Changing material, dimensions, or packaging after sample approval without revalidation. A seemingly small change can affect resistance, fatigue, printing, fit, or shipping readiness.
Buyer checklist before sample approval
- What exact product construction are we buying? Material and manufacturing method affect feel, elongation, appearance, and test behavior.
- At what extension will resistance be measured? Force data is not comparable unless the extension and method are defined.
- What force range and tolerance applies to every level? This prevents different batches or colors from overlapping unexpectedly.
- What fatigue setup will be used? Record extension ratio, cycle count, speed, environment, and failure criteria.
- Are we testing the material or the final assembly? Products with handles or attachments require verification of their connection points.
- What width and thickness tolerances apply? LBP’s general references are width +/-5% and thickness +/-0.3 mm unless the order establishes another written specification.
- Which defects are critical, major, and minor? Written definitions and reference photographs make inspection decisions repeatable.
- What AQL and inspection level will govern lot acceptance? The defect AQL alone does not determine the sample size.
- What evidence is required before shipment? Agree on test photographs, measurement summaries, packing photographs, and inspection results that can be shared.
- What must trigger reapproval? Material, construction, dimensions, resistance, attachments, artwork, and packaging changes should be controlled.
What to send for an accurate quote
For a faster technical review, send:
- product type and intended application;
- target market and sales channel;
- material preference;
- dimensions and tolerances;
- resistance range at a stated extension;
- fatigue-cycle target and test conditions;
- color or Pantone references;
- logo artwork and printing requirements;
- packaging, barcode, inserts, and carton requirements;
- estimated sample and order quantities;
- desired inspection or AQL requirements;
- target delivery date.
Final recommendation
The strongest private-label program starts with a specification both sides can test. Use the approved sample to define appearance and feel, then support it with measurable force, dimensions, fatigue, defects, packaging, and lot-acceptance requirements.
LBP Fitness develops custom resistance bands and private-label resistance-band programs for brand and OEM buyers. Send us your target dimensions, resistance levels, branding, packaging, and test requirements for a sample-development and quality-control review.
External technical references
- ASTM D412, Standard Test Methods for Vulcanized Rubber and Thermoplastic Elastomers—Tension: https://store.astm.org/standards/d412
- ISO 2859-1:2026, Sampling procedures for inspection by attributes: https://www.iso.org/standard/85464.html
- US CPSC, HomeProGym resistance-band recall, May 21, 2026: https://www.cpsc.gov/Recalls/2026/Resistance-Bands-Recalled-Due-to-Serious-Injury-from-Impact-Hazard-Imported-by-HomeProGym
- US CPSC, SPRI resistance-band recall: https://www.cpsc.gov/Recalls/2020/Fit-For-Life-Recalls-SPRI-Ultra-Heavy-Resistance-Bands-Due-to-Injury-Hazard